If you’ve ever spec’d components for mining, construction, aggregate processing, or heavy agriculture, you’ve almost certainly come across abrasion resistant (AR) steel. As someone who’s supplied AR steels to fabricators and manufacturers across North America for over a decade, one question I get asked more than any other is: “Can I actually machine this stuff without wrecking my tools, blowing out my budget, or ending up with a part that doesn’t fit?” The short answer is yes—but it’s not like machining mild steel. AR steel isn’t some mysterious “unmachinable” material, but it’s not your run-of-the-mill low-carbon A36 either. It’s designed to outlast standard steel when grit, debris, and constant friction are at play, and that durability comes from a unique metallurgical makeup that changes how every step of fabrication works. Let’s break this down, because if you skip the right approach, you won’t just get bad parts—you’ll waste time, money, and good tooling. Abrasion Resistant Steel
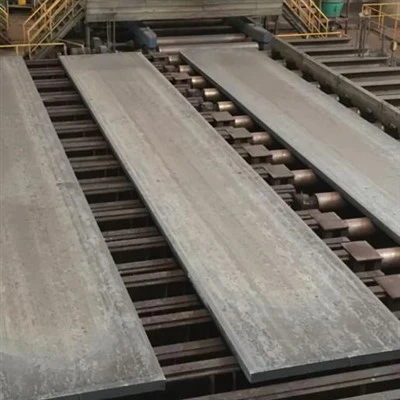
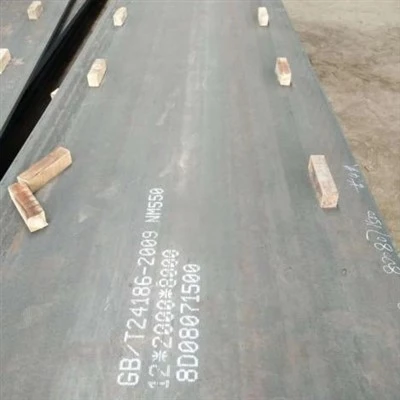
First, let’s get one thing straight: not all AR steel is the same. I’ve seen fabricators show up to my shop with a piece of 400 Brinell (BHN) AR 400 thinking it’s identical to their old A36 plate, and within an hour, they’ve burned through a $150 end mill and stripped a tap. The most common mistake is treating all AR steel like one product. AR steels are classified by their Brinell hardness rating: numbers like 400, 450, 500, up to 550 BHN for the hardest grades. The higher the BHN, the more abrasion resistant the steel—and the harder it is to machine. For reference, mild A36 steel clocks in around 120 BHN, so even the softest AR steel is three times harder than what most fabricators work with daily. That difference isn’t trivial. The hardness comes from a microstructure of tempered martensite, a fine, strong crystalline structure formed when the steel is quenched during manufacturing. Unlike high-carbon tool steel, which is often soft before heat treatment and hardened after machining, AR steel is almost always delivered in its final, hardened state. That means you’re not cutting soft steel then hardening it—you’re cutting hardened steel, which is a totally different process.
So, why is machining AR steel different? Let’s start with tooling. When you cut metal, the tool’s job is to shear the material away cleanly. With soft steel, a standard high-speed steel (HSS) tool will work fine, because the material yields and flows rather than resisting. With hardened AR steel, the material is so strong that it doesn’t yield—it chips. That puts enormous pressure on the cutting edge of the tool, which will wear out extremely fast if it’s not designed for this job. I always tell my customers that for any machining on AR steel, skip HSS tools entirely. Stick with solid carbide or coated carbide tools, and make sure the coating is optimized for hard materials. Titanium aluminum nitride (TiAlN) coatings are the gold standard here—they can handle the high heat generated when cutting hardened steel, resist abrasion from the steel’s martensite structure, and extend tool life by 200-300% compared to uncoated carbide. For even harder grades (500 BHN and up), some fabricators use polycrystalline cubic boron nitride (PCBN) tools, though those are more expensive and usually only worth it for high-volume production runs where tool change downtime adds up. One trick I’ve learned over the years: use tools with sharper, honed edges, not rounded ones. Rounded edges generate more friction and heat, which causes both tool wear and premature failure. I once had a customer bring in a set of parts he’d machined with worn, rounded end mills—he ended up needing to scrap 12 parts because the cuts were too rough, and he’d spent three times more on tooling than he would have if he’d used sharp, coated carbide bits from the start.
Next up is machining parameters. A lot of guys new to AR steel think, “It’s harder, so I’ll just slow down the speed.” That’s wrong. When cutting hardened steel, heat is your enemy—but so is friction. If you slow your cutting speed too much, the tool will rub against the steel instead of cutting it, building up heat that will soften the tool’s edge and cause crater wear or chipping. The sweet spot for AR steel is usually a cutting speed that’s 50-70% of what you’d use for a mild steel of the same hardness, and a feed rate that’s slightly higher. Wait, let me rephrase that clearly: for example, if you’d run an end mill at 150 surface feet per minute (SFPM) for A36, run it at 75-100 SFPM for AR 400, not 50. The higher feed rate means the tool is cutting through the material instead of scraping it, which reduces both heat and tool pressure. Depth of cut matters too. Don’t take full, deep passes in one go. AR steel is prone to vibration (also called chatter) if you’re taking too thick a chip, especially with long tools like end mills. I recommend using multiple light passes—half the depth you’d use for mild steel—instead of one deep pass. It adds a tiny bit of cycle time, but it keeps your cuts consistent, extends tool life, and avoids damaging the part. Coolant is another big one. Not just any coolant—use a high-pressure, high-flow synthetic coolant designed for hard machining. Flood coolant works, but through-tool coolant, where the coolant is pumped directly through the tool to the cutting edge, is even better. It keeps the tool edge cool, flushes away chips so they don’t get caught between the tool and the part, and reduces friction. I’ve seen fabricators skip coolant “to save money” and end up with tools that last 10 minutes instead of an hour—total false economy.
Now, what about specific machining operations, because AR steel behaves differently depending on what you’re doing. Let’s start with turning. Turning cylindrical parts—like rollers, shafts, or bushings—on a lathe is one of the most common machining jobs for AR steel. For turning, you want to use a rigid lathe, no wobble, because vibration is even more of an issue here than with milling. Use a positive rake angle insert—positive rake cuts through material with less force, which reduces chatter and tool stress. For turning AR 400, a carbide insert with a TiAlN coating will work perfectly; for AR 500 or higher, PCBN inserts are a better bet. Drilling is another big one. Drilling AR steel is notoriously tricky because chips can get stuck in the flutes of the drill, causing it to break or walk across the part. The solution here is a drill with a split point (also called a 135-degree point angle) — it won’t wander like a standard 118-degree drill, and it cuts through the hardened steel cleaner. Use a slow feed rate, and plenty of through-drill coolant if your machine has it. I’ve had customers drill holes in AR 500 with a standard HSS drill and break three bits—switch to a TiAlN-coated carbide drill, and they’ll drill 20 holes with no issues. Milling is the operation most people struggle with, because end mills are longer and more prone to chatter. Use short, rigid end mills whenever possible—skip the long, lightweight ones for AR steel, even if you have to clamp the part closer to the vise. For slotting or side milling, climb milling (where the tool rotates in the same direction as the part feed) instead of conventional milling. Climb milling reduces friction between the tool and the work material, minimizes chatter, and gives a smoother finish. Just make sure your machine has adequate backlash control, because climb milling can cause backlash issues if your table is loose. And if you need to do tapping? Yes, you can tap AR steel—just use a spiral flute tap, not a straight flute tap. Spiral flutes pull the chips out of the hole instead of packing them in, which prevents tap breakage. Tap at a slower speed than you’d use for mild steel, and use a tapping oil designed for hard materials—straight cutting oil works better than general-purpose coolant here.
Wait, but what about the finish of the part, and its durability? I get this question all the time from customers: if I machine AR steel, will the machined area be as abrasion resistant as the plate? The short answer is no, but that’s not a bad thing. When you machine AR steel, the heat and pressure from the cutting process can create a tiny layer on the surface called a white layer, or a heat-affected zone (HAZ). This layer is harder than the base material, but it’s also brittle—more prone to cracking and chipping under impact or abrasion. The good news is that this layer is extremely thin, usually only a few thousandths of an inch, and it’s easily removed during secondary operations like grinding or blasting. If you’re spec’ing a part that will be exposed to heavy abrasion, just plan to grind the machined surfaces smooth after machining, or allow for a small amount of extra material (0.010 to 0.020 inches) to be removed in a final pass to get rid of the white layer. I always recommend that to my customers, because it prevents premature failure of the machined part in the field.
Now, let’s talk about common myths that I’ve heard over the years. First myth: “AR steel is too hard to machine, so I should use a softer grade and add hardfacing later.” Wait a minute—hardfacing is great for extreme applications, but it’s expensive, time-consuming, and not as uniform as AR steel. Machining AR steel correctly is faster and more cost-effective than hardfacing a part. Another myth: “You can’t use standard CAD/CAM software for AR steel.” No, you just need to adjust the cutting parameters—most modern CNC software has pre-built parameter libraries for AR steel, so you just select the grade you’re working with, and it adjusts speed, feed, and depth of cut automatically. I’ve also heard, “It causes excessive tool wear, so it’s not worth the hassle.” Tool wear is a thing with any material, but the difference is that with AR steel, if you follow the right process, tool life is predictable, and the parts you make will last 2-5 times longer than parts made from mild steel. That ROI is huge for customers who are buying parts for mining or construction, where downtime costs thousands of dollars per hour.
I’ve seen this play out so many times with my own customers. Early in my career, I had a customer who made bucket teeth for excavators. He was using A36 steel for the teeth, and they were wearing out in six months on his jobsite. He switched to AR 400, and he thought he couldn’t machine it, so he sent it to a local fabricator who burned through tooling and quoted him 30% more than he was paying for A36. I sat down with him, walked him through the right tooling, parameters, and operations, and he started machining it in-house. His tooling costs went up by 15%, but the bucket teeth lasted 18 months. Over a year, he saved $45,000 in replacement costs and downtime. That’s the value of doing it right.
So, to wrap this up: yes, abrasion resistant steel can absolutely be machined—you just have to treat it like the specialized, high-performance material it is, not just a thicker or harder version of mild steel. The key steps are: use tooling designed for hard, abrasive materials (coated carbide, TiAlN coatings, sharp edges), adjust your cutting parameters to run slightly lower speeds and higher feeds with light, multiple passes, use high-pressure coolant to keep the tool and part cool, and plan to remove the tiny brittle heat-affected zone after machining if your part will see heavy abrasion. Skip the shortcuts—don’t use HSS tools, don’t run slow enough to rub instead of cut, don’t skip coolant—and you’ll get consistent, high-quality parts that stand up to the extreme conditions your customers need.
If you’re working on a project that uses AR steel, whether you’re fabricating parts for mining, agriculture, material handling, or any other heavy-duty application, and you’re not sure where to start with machining, I’d be happy to walk you through the specifics for your grade, part, and operation. As a supplier, my job isn’t just to sell you steel—it’s to help you use it correctly, so your parts perform as intended and you avoid costly mistakes. Reach out to discuss your project, and we can work together to make machining AR steel straightforward and cost-effective for your operation.
EN High Strength Steel Plate References
ASM International. (2019). Properties and Selection: Irons, Steels, and High-Performance Alloys. ASM Handbook, Volume 1.
Klocke, F., & König, W. (2008). Manufacturing Processes 2: Grinding, Honing, Lapping. Springer.
Metal Cutting Tooling Institute. (2021). Machining Abrasion Resistant Steels: Best Practices for Fabricators. MCTI Technical Bulletin 412.
Gnee Steel (Tianjin) Co., Ltd.
As one of the most professional abrasion resistant steel manufacturers and suppliers in China, we also support customized service with low price. We warmly welcome you to buy high quality abrasion resistant steel in stock here from our factory. If you have any enquiry about free sample, please feel free to email us.
Address: No.4-1114, Beichen Building, Beicang Town, Beichen District, Tianjin, China
E-mail: alloy@gneesteelgroup.com
WebSite: https://www.chinavesselplates.com/
